
Introduction — Where the Shop Floor Meets the Data
Have you ever watched a job sit idle because the control wouldn’t behave? I see that scene a lot: a bench full of parts, a planner on the phone, and a machinist waiting. CNC milling and turning centers sit at the heart of that moment—machines, software, and people all trying to pull in the same direction. Recent shop surveys (I keep a stack of them) suggest downtime and setup drift still eat 20–35% of productive hours on many floors. So what really breaks productivity: hardware limits, interface confusion, or poor integration?

Let me be blunt: the answer rarely lives in a single cause. It’s usually a chain — bad handoff from CAM, a control that buries key settings, or simple axis backlash that refuses to behave. We’ll walk through where systems fail, and what to watch for next. — onward to the control layer.
Deep Dive: Where syntec control system cnc Runs Up Against Reality
syntec control system cnc is popular because it’s affordable and familiar. I’ve used it on lathes and combos, and I’ve seen it shine — and stumble. When I say stumble, I mean issues like sluggish M-code responses, confusing tool offset screens, and limits in multi-axis interpolation that show up during complex cycles. These are not just annoyances. They cost minutes — sometimes hours — per job. Servo turret misalignment, spindle speed lag, and encoder noise are common culprits. Look, it’s simpler than you think: if the control doesn’t expose clear diagnostics, the first-hour troubleshooting becomes a treasure hunt.
What fails first?
Technically, the weak spots are repeatability-related: axis backlash, poor encoder feedback, and inconsistent tool offset handling. I’ve measured part-to-part scatter that points back to the control’s handling of compensation tables. The syntec control system cnc can mask these faults when default settings are left unchanged. Worse, many shops lack simple monitoring like real-time spindle load or turret torque traces. When I recommend fixes, they are basic: tighten encoder grounding, verify tool offset tables after regrind, and use conditional logging to capture spindle speed variations. Those steps take time but return repeatability fast.
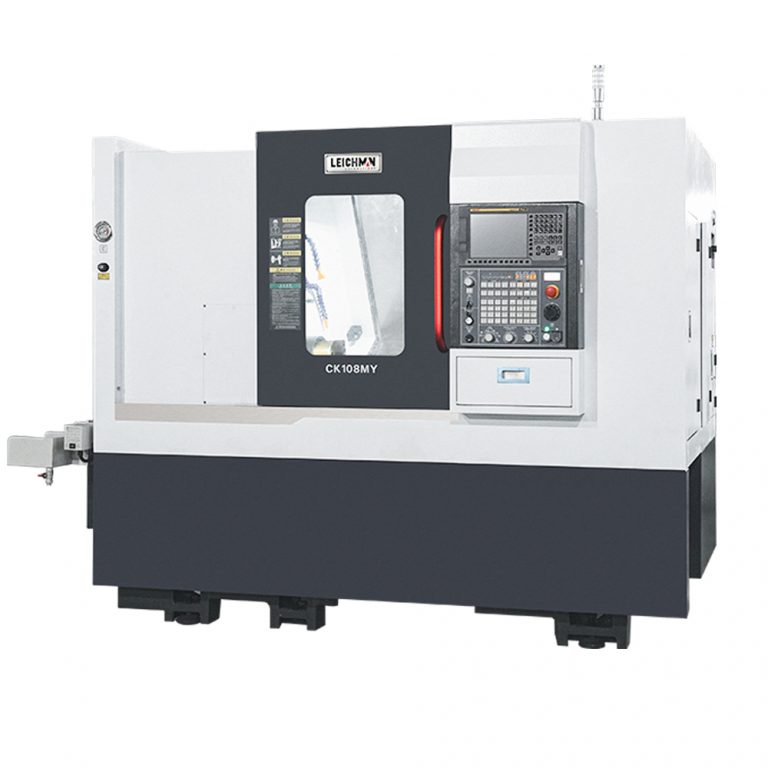
Forward View: Principles for New Builds and Retrofit Choices
What if we stop chasing band-aid fixes and pick principles instead? I prefer to think in building blocks: clear HMI, deterministic motion control, and robust I/O for sensors. For small shops moving to a hybrid cell, a modern milling and turning machining center with y axis changes the playbook. With Y-axis capability you reduce setups, cut cycle times, and simplify tooling. But — funny how that works, right? — the added axis raises the bar for control quality and tuning.
What’s Next for decision-makers?
Start with interoperability: can the control talk cleanly to your CAM post-processor and MES? Then look at motion fidelity: does the servo loop support tight gains without hunting? Finally, don’t ignore ergonomics — a well-laid HMI reduces input errors more than tighter tolerances ever will. In practice, I’ve seen shops pick the right mix by doing two small pilots rather than a single wholesale swap. One pilot tests the control’s diagnostics and logging; the other validates a tool-change and probing cycle under normal shift conditions. Both gave practical answers fast.
To help you choose, here are three metrics I trust when evaluating a control or machine: 1) Closed-loop accuracy under load (microns at spindle torque), 2) Time-to-first-good-part (minutes from program start), and 3) Diagnostic transparency (ease of reading encoder, servo, and spindle traces). Use those. They tell you what actually matters on the floor — measurable, not marketing-speak. We’ve used this checklist in shops where margin was tight and results were immediate. If you want a practical partner for machines and retrofits, check out Leichman.